 Chart 01
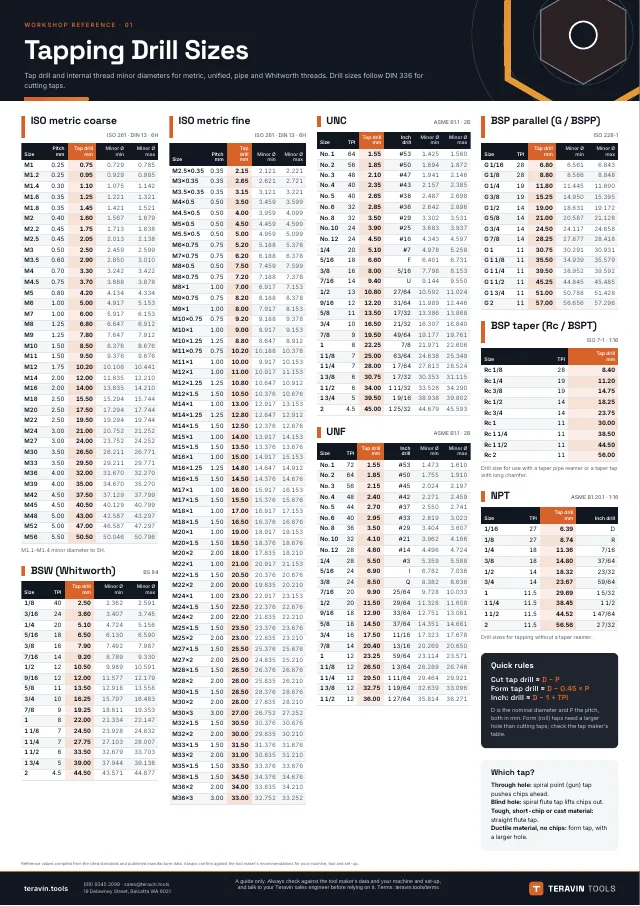
Tapping Drill Sizes
Tap drills and internal thread minor diameters for metric, unified, pipe and Whitworth threads.
Twelve A3 reference charts for the shop floor. Download one, or the whole set, and print it for the wall next to the machine.
Chart 01Tap drills and internal thread minor diameters for metric, unified, pipe and Whitworth threads.
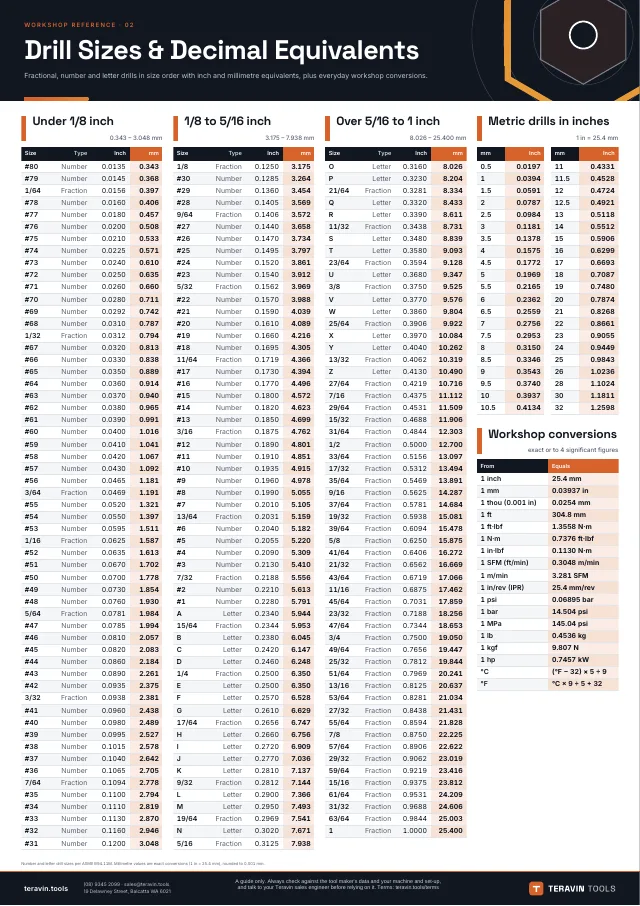 Chart 02
Fractional, number and letter drills in size order with inch and millimetre equivalents.
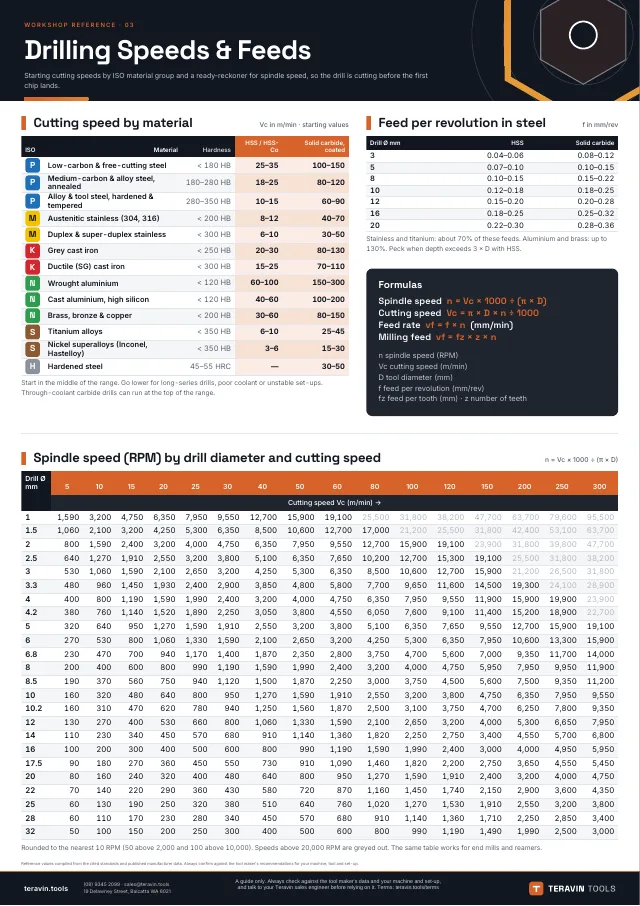 Chart 03
Starting cutting speeds by ISO material group and a spindle speed ready-reckoner.
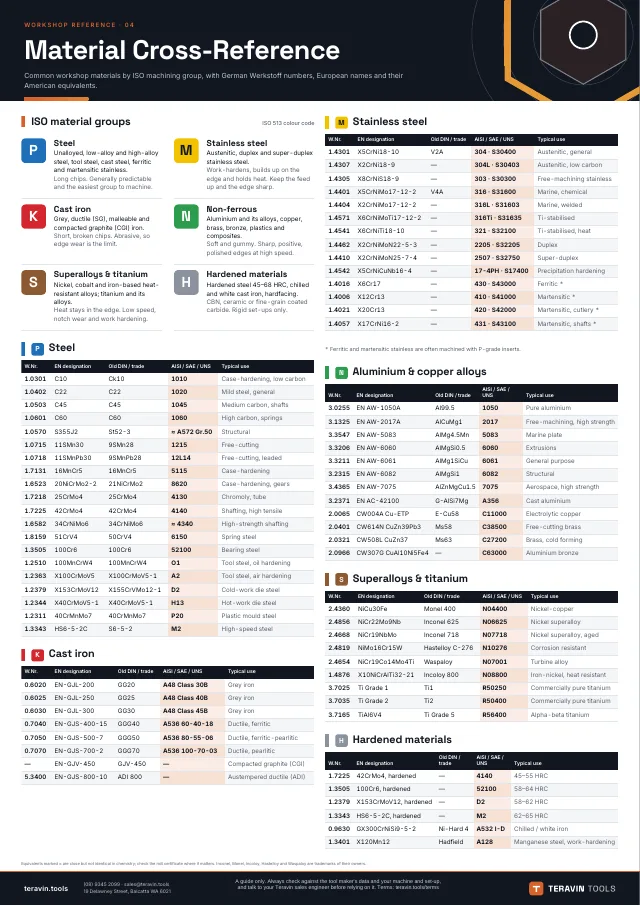 Chart 04
Common workshop materials by ISO group, with Werkstoff numbers, European names and American equivalents.
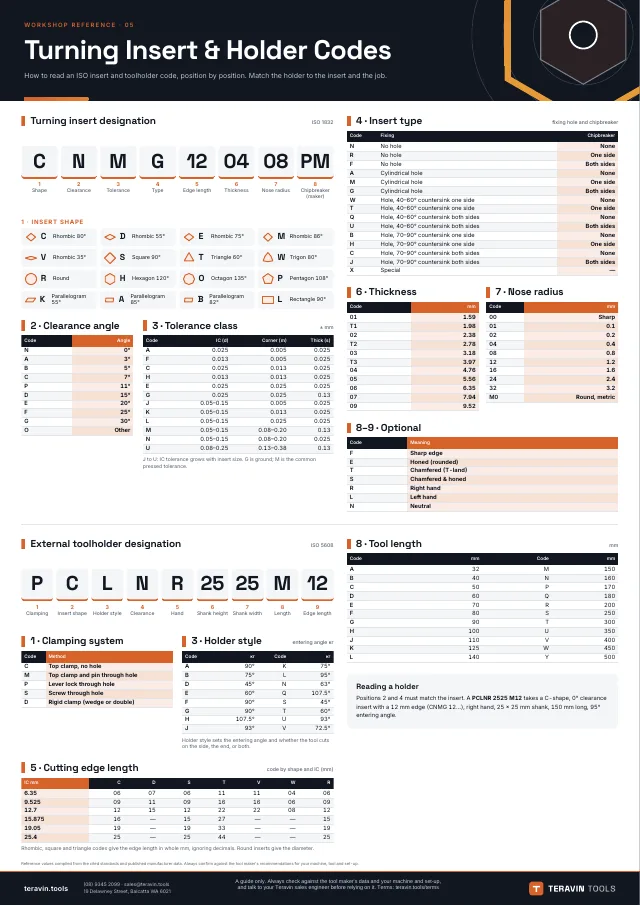 Chart 05
How to read an ISO insert and toolholder code, position by position.
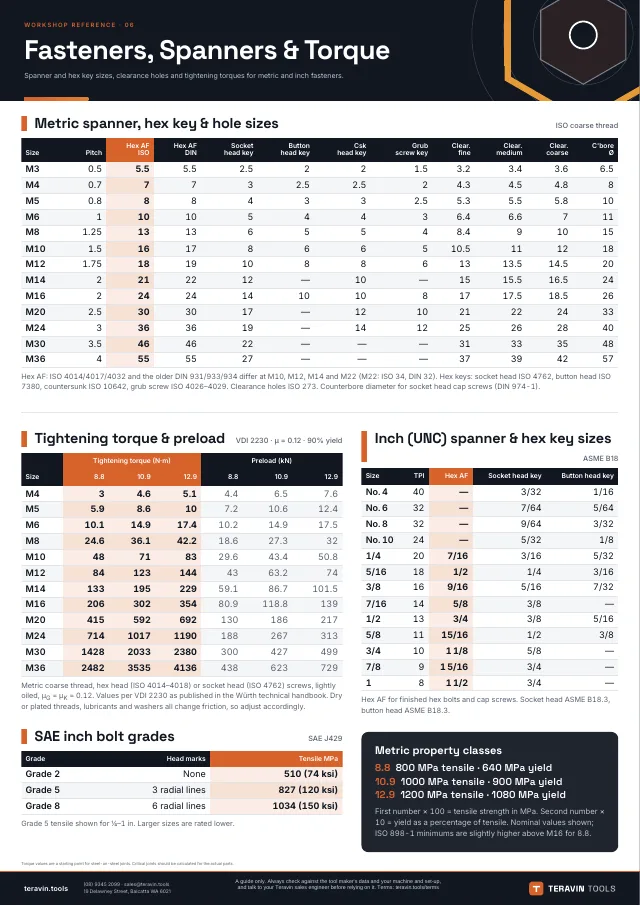 Chart 06
Spanner and hex key sizes, clearance holes and tightening torques for metric and inch fasteners.
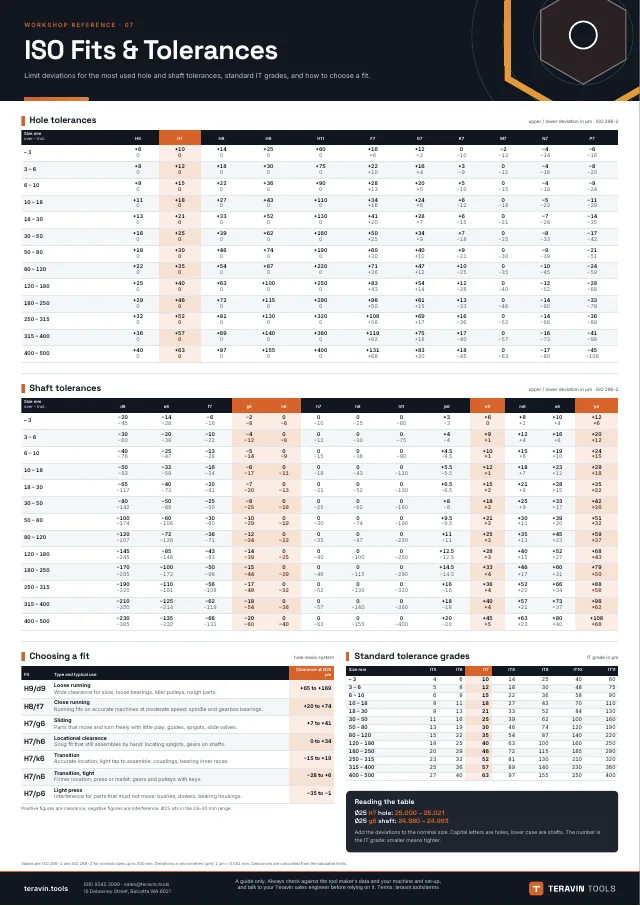 Chart 07
Limit deviations for the most used hole and shaft tolerances, IT grades and choosing a fit.
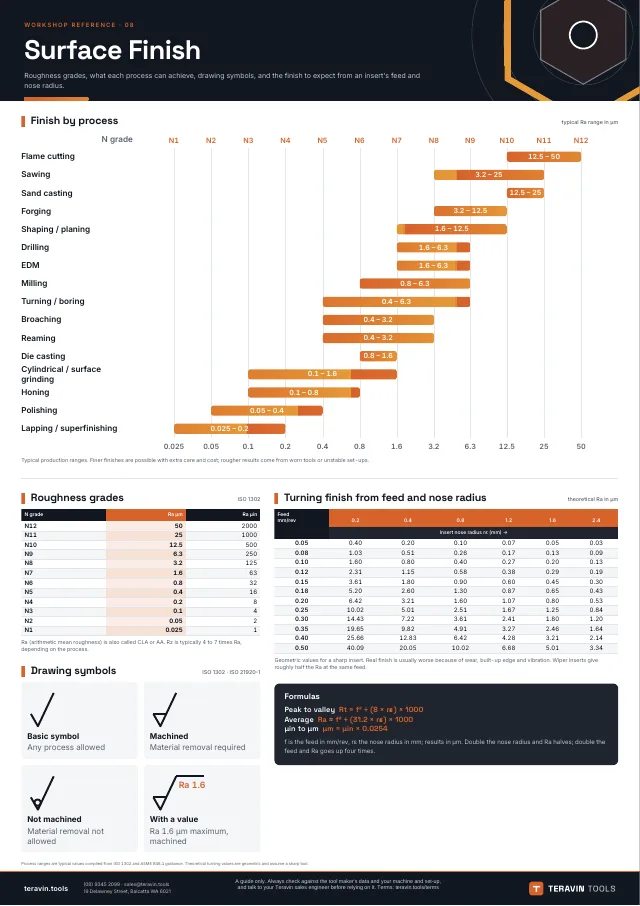 Chart 08
Roughness grades, what each process can achieve, drawing symbols and finish from feed and nose radius.
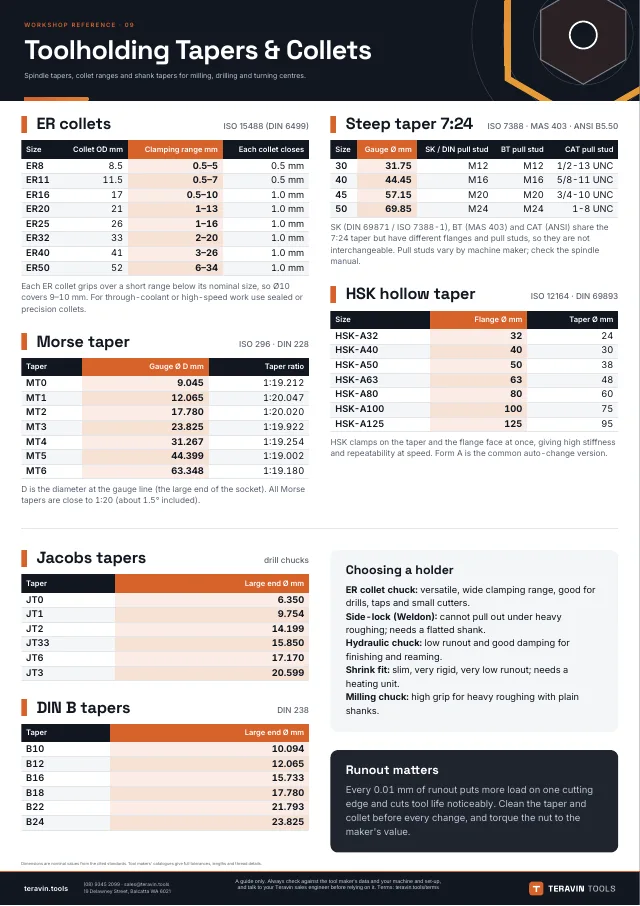 Chart 09
Spindle tapers, collet ranges and shank tapers for milling, drilling and turning centres.
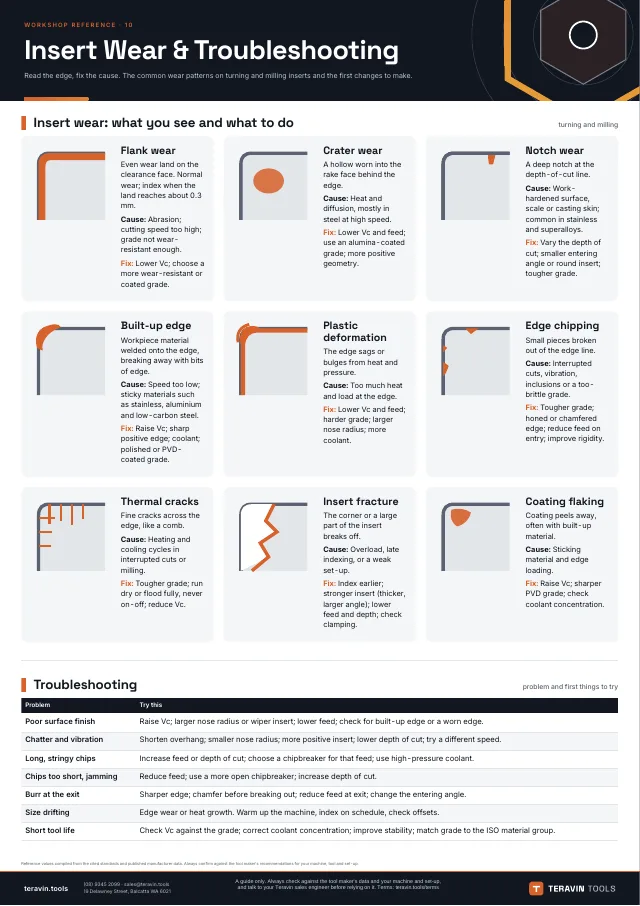 Chart 10
The common wear patterns on turning and milling inserts and the first changes to make.
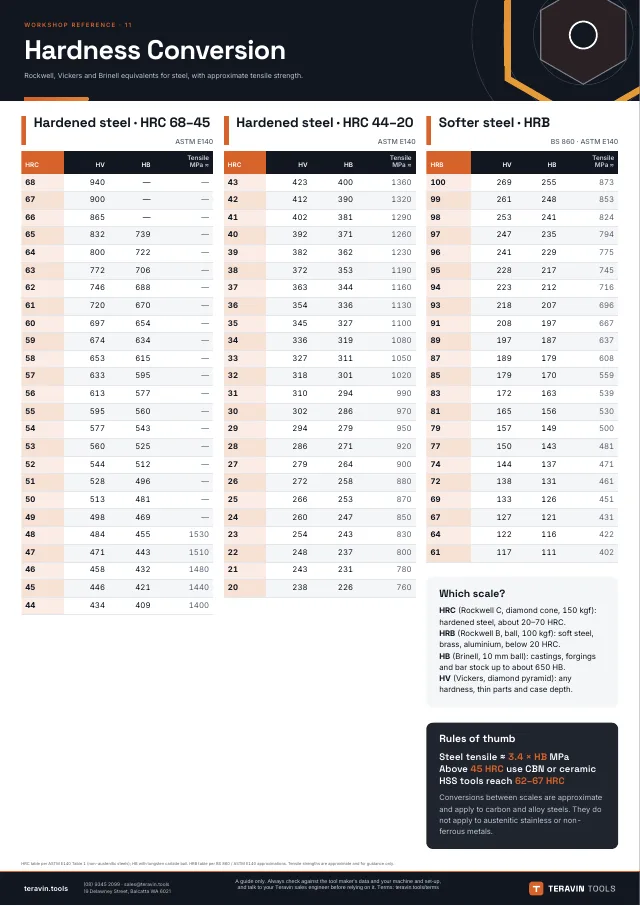 Chart 11
Rockwell, Vickers and Brinell equivalents for steel, with approximate tensile strength.
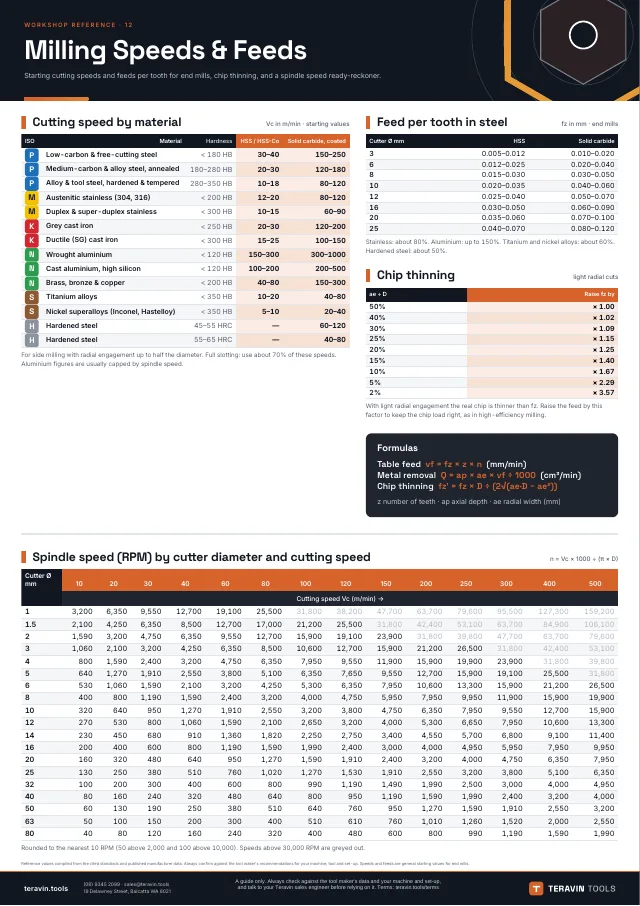 Chart 12
Starting cutting speeds and feeds per tooth for end mills, chip thinning and a spindle speed ready-reckoner.
Charts are for general workshop reference. Always check the tool maker’s catalogue for exact cutting data. Want a printed set for your workshop? Ask us.
A guide only. These tools and figures are general starting points, not a guarantee for your job. Results depend on your machine, setup, material and tooling, so always check against the tool maker’s data, and talk to a Teravin sales engineer to make sure it’s right for your application. Call +61 8 9345 2099 or ask us. See our terms of use.